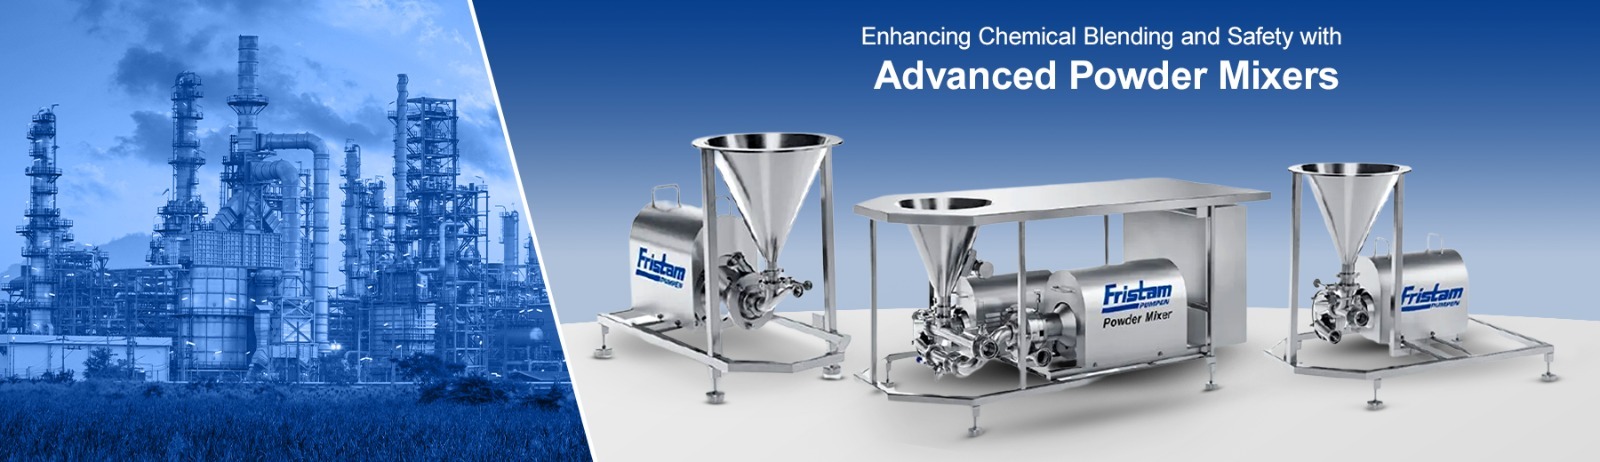
Enhancing Chemical Blending and Safety with Advanced Powder Mixers
September 29, 2025
 In the chemical industry, blending powders into liquids is a critical step that impacts product quality, efficiency, and workplace safety. Many plants still struggle with inefficient processes, wasted materials, and safety risks. That’s why businesses are turning to advanced powder mixers, designed to improve mixing efficiency in chemicals while keeping operators safe.
Let’s look at how modern chemical blending technology helps achieve these goals and why Fristam’s solutions stand out in the market.
Why Chemical Blending Needs Advanced Technology
Blending powders into liquids sounds simple, but in practice, it’s complex. Traditional methods like manual mixing or simple tank agitators often lead to clumps, uneven distribution, or wasted materials. Worse, they expose workers to dust, spills, and strain. Advanced powder mixers solve these issues by using precise engineering and smart powder blending techniques. They ensure powders dissolve quickly and evenly, reduce material loss, and improve workplace hygiene and safety.Key Benefits of Advanced Powder Mixers
1. Higher Efficiency Modern powder mixing systems are designed for speed and accuracy. They minimize mixing time while achieving consistent, homogeneous results. This means fewer batches fail, saving both time and money. 2. Better Safety in Powder Handling One of the biggest challenges in the chemical industry is operator safety. Advanced mixers are built at ergonomic heights and eliminate the need for climbing or lifting heavy bags. This lowers the risk of injury and prevents dust exposure – a key aspect of safety in powder handling. 3. Consistent Quality High-performance mixers deliver uniform textures and prevent clumps or residue. With improved mixing efficiency in chemicals, manufacturers can ensure product quality and meet stringent industry standards. 4. Versatility Innovative blending solutions handle a wide variety of powders, from highly soluble to challenging, less-soluble materials, and work seamlessly with liquids of different viscosities.Why Choose Fristam’s Powder Mixers?
Fristam is a trusted powder mixer manufacturer and supplier, offering a complete range of high-performance powder mixers tailored to the needs of the chemical and related industries. Here are our three standout solutions: PM / PMV Powder Mixer Meticulously designed to blend wet and dry ingredients seamlessly, the PM / PMV mixers dissolve, emulsify, and homogenize powders into liquids effectively.- Hygienic and CIP/SIP compatible
- Available in 5 sizes for PM and 3 sizes for PMV
- Powder intake up to 10 tons per hour
- Ergonomic table for safe, floor-level operation
- Compact design with ergonomic height
- High-speed shearing (up to 38 m/s)
- Consistent homogeneity, every time
- Fast intake of large powder volumes
- Floor-level design improves safety and efficiency
- Reduces labour and material costs significantly